Welcome to Metallurgical Hengtai (Tianjin)Technology Co.,Ltd
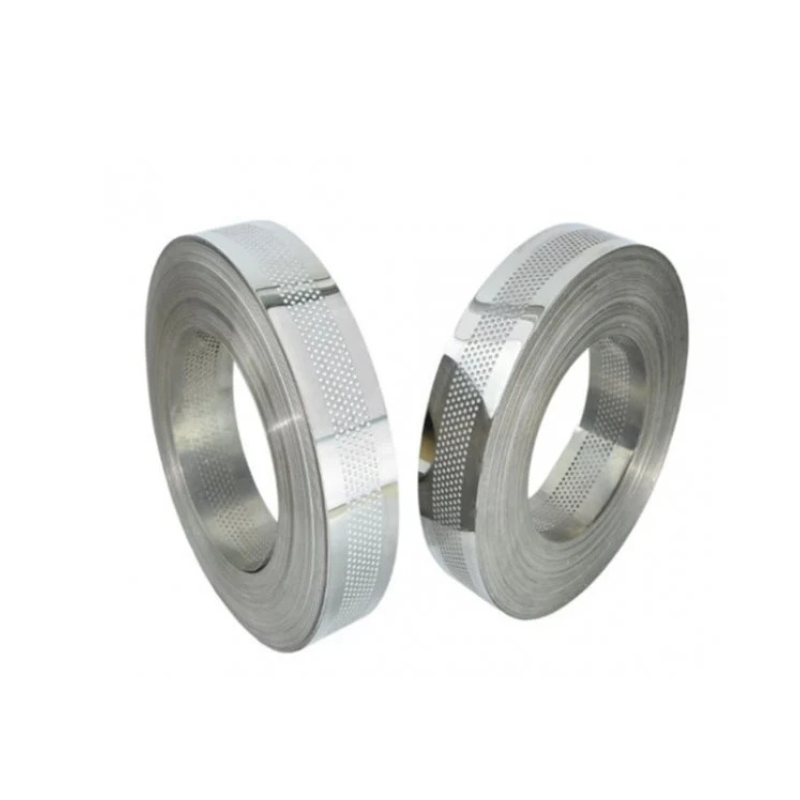
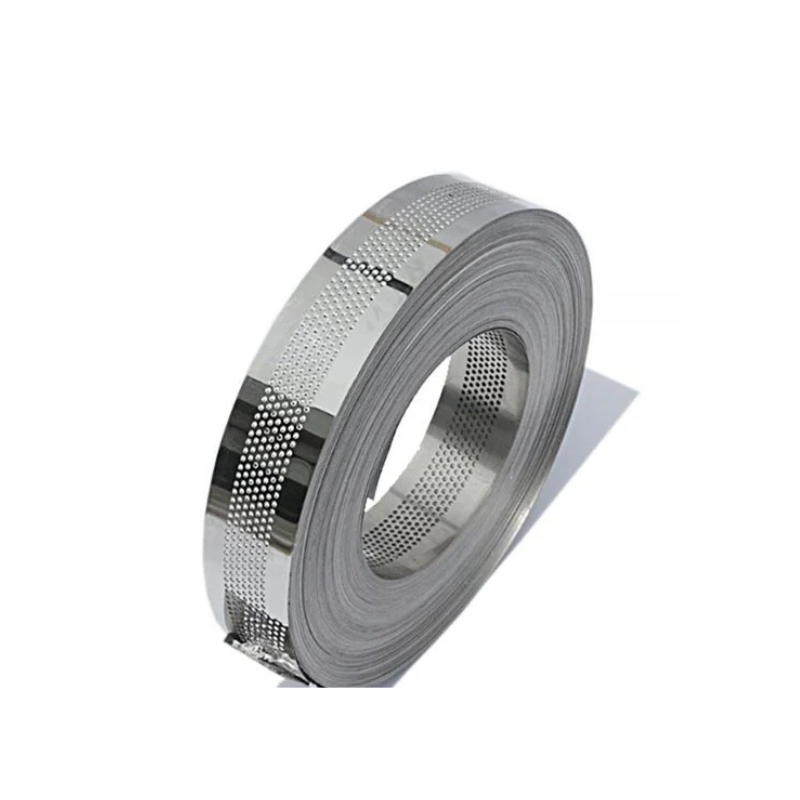
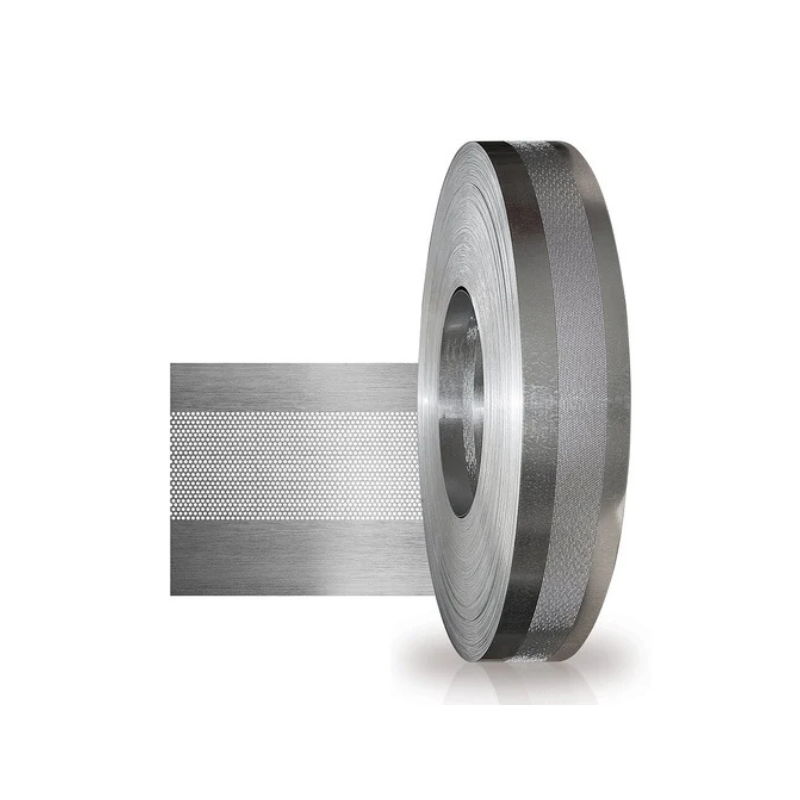
Perforated metal strip
Perforated Metal Strip — The Pattern Is Only Half the Specification
Narrow perforated strip in coil — round, square or slotted patterns, perforated continuously or in repeating registers with solid lands between, slit to width and finished for your press or forming line.
Almost every enquiry for perforated strip arrives with a hole pattern. Very few arrive with the coil specification, and it is the coil specification that decides whether the strip runs on your line or stops it. A perforated coil is not a stack of sheets in a different shape: your feeder pulls it, your pilots locate it, and your press cycles at rate. So along with the pattern, what has to be defined and held is coil inner and outer diameter, coil weight, strip width and thickness, the linear length you need, and whether that length is one continuous run or contains welds.
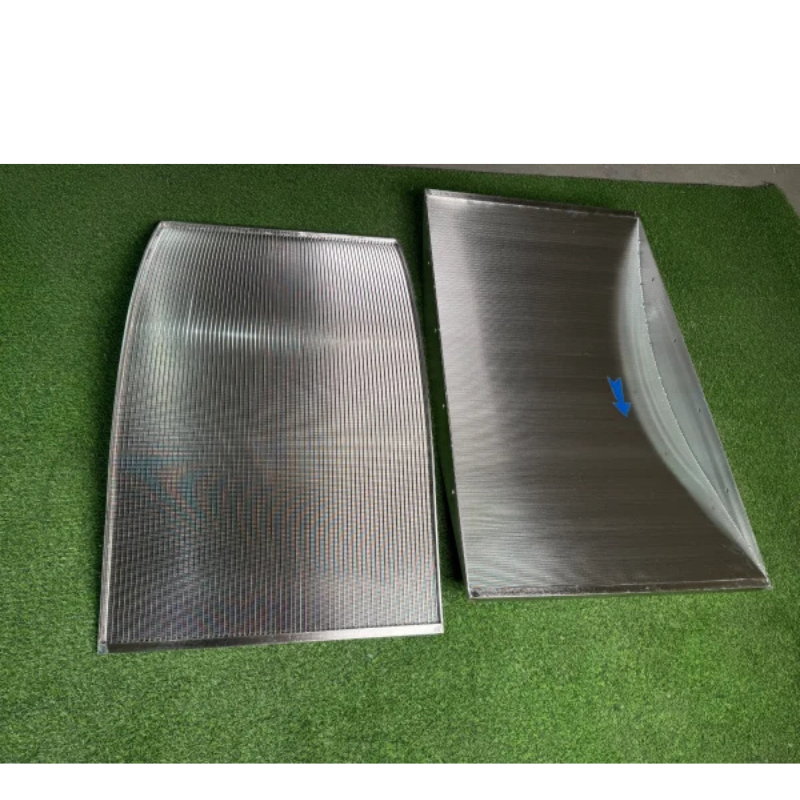
The number that most often decides success is register accuracy. Where a strip is perforated in repeating zones with solid lands between them — as in the photo — your tooling indexes on those zones. Each perforated window has to sit at the right position along the coil, at the same repeat pitch, from the first metre to the last. A window that drifts out of register does not announce itself; it feeds slightly wrong, and you find it as scrap or as a stopped press. The second number is camber. Perforating does not remove material evenly across a strip, so the coil has a natural tendency to bow sideways, and lateral bow is the most common reason a coil-fed strip will not run straight through a guide. We measure and declare camber per coil, and we will tell you what the pattern you have chosen is likely to do to it before you commit to tooling.
Specification at a glance
| Form | Perforated strip in coil;also supplied as spooled or cut lengths |
| Perforation layout Register | Continuous perforation,or repeating registers with solid lands between (skip perforating)—to your drawing Window length and repeat pitch to your drawing; position tolerance declared per coil |
| Pattern | Round, square, slotted;60°staggered or straight grid |
| Aperture | [0.5]-[10] mm |
| Open area | [10]-[60]% within the perforated zone |
| Strip width | [6]-[600]mm,slit to width |
| Thickness | [0.1]-[3.0]mm |
| Camber | Measured and declared per coil |
| Joins | Single continuous length,or welded coils with weld positions declared and marked on the coil Inner diameter [3001400/508]mm,weight and coil tension set for your line |
| Materials | Cold rolled and galvanized steel,stainless 304/316L,aluminium,brass and copper |
| Finish and packing | Bright or polished finish interleaved to protect the face in transit;coated options on request |
| Documents | EN 102043.1 MTC,dimensional and register record,weld position record,packing list,B/L, certificate of origin |
Why buyers run their strip from here
Register documented, not assumed. Window position and repeat pitch are recorded per coil, so what you qualified is what your feeder indexes on in production.
Camber measured and declared. Lateral bow is stated per coil rather than discovered at the feeder, which is the difference between a settled run and an afternoon of scrapped strip.
Welds declared and marked. Where a coil contains joins, their position is recorded and flagged on the coil itself, so a hard spot never arrives unannounced at your die.
Bright faces protected. Interleaving and coil tension set for a reflective or polished finish, so the strip arrives with the face you inspected.
Send your pattern drawing or sample, aperture and register dimensions, strip width, thickness, material, finish, plus the coil size and linear length your line requires. We will confirm register capability and camber, quote FOB [Tianjin] and give you a lead time — usually within [24] hours.